
1. Product Overview
Potassium Hydroxide (KOH), also known as caustic potash, is a highly alkaline inorganic compound supplied primarily as solid flakes, pellets, or other industrial-grade forms. It is widely used in chemical manufacturing, detergents, fertilizers, water treatment, petroleum processing, and various industrial synthesis applications. Its strong alkalinity, high reactivity, and excellent solubility make it a versatile processing chemical for demanding industrial operations. As a critical chemical feedstock, KOH supports efficient production processes and reliable large-scale industrial manufacturing.
2. Key Specifications & Technical Characteristics
- Chemical Composition: Potassium Hydroxide (KOH)
- Typical Purity: Industrial grade, commonly supplied at approximately 90–99% KOH depending on specification
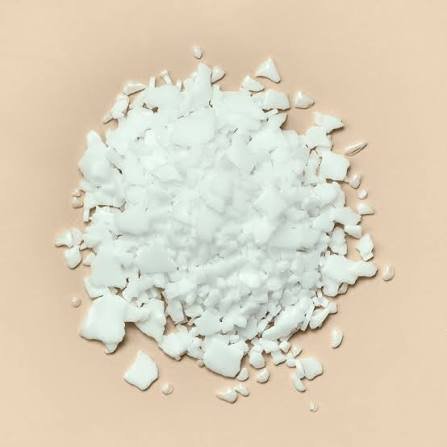
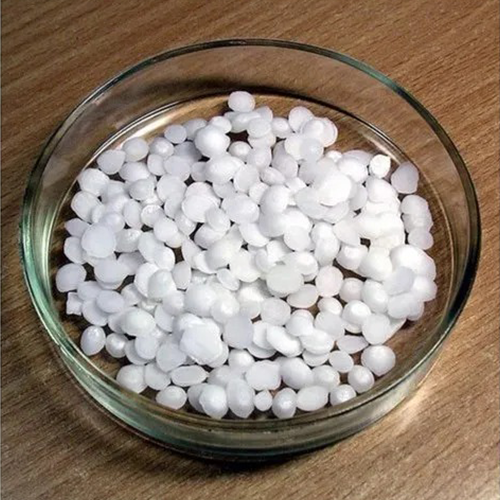
- Physical Form: White or off-white flakes, pellets, or solid material
- Solubility: Highly soluble in water, generating significant heat during dissolution
- Alkalinity: Strong inorganic base with high chemical reactivity
- Packaging Options: 25 kg bags, 500–1,000 kg jumbo bags, or bulk packaging subject to supply requirements
- Shelf Life: Typically up to 24 months when stored in tightly sealed, moisture-resistant packaging under suitable conditions
- Storage: Keep dry and tightly sealed; protect from moisture, acids, and incompatible materials
- Origin: Available from established international chemical supply sources, subject to buyer specification and sourcing requirements
3. Core Industrial Applications
- Chemical Manufacturing: Used as a fundamental alkaline reagent and feedstock in the production of potassium-based chemicals, salts, and specialty compounds.
- Detergents & Cleaning Products: Provides strong alkalinity for soaps, liquid detergents, industrial cleaners, and degreasing formulations.
- Water Treatment: Supports pH adjustment and neutralization processes in industrial water and wastewater treatment systems.
- Fertilizer Production: Used in the manufacture and processing of potassium-containing agricultural inputs.
- Petroleum & Refining: Applied in selected refining, gas treatment, and chemical processing operations requiring a strong alkaline reagent.
- Battery & Specialty Chemical Processing: Used in selected manufacturing and processing applications where controlled potassium chemistry and high alkalinity are required.
Its high solubility and strong, consistent alkalinity enable efficient reaction control, rapid formulation, and reliable process performance compared with weaker alkaline alternatives.
4. Competitive Advantages
- Quality Consistency: Consistent chemical composition and reliable alkaline performance for industrial-scale processing.
- Supply Reliability: Suitable for bulk procurement programs and recurring industrial supply requirements.
- Logistics Capability: Flexible packaging and bulk-loading options designed to support international B2B distribution.
- Price Competitiveness: Bulk sourcing provides opportunities for cost-efficient procurement and optimized supply economics.
- Operational Efficiency: High solubility and strong alkalinity support efficient processing and formulation.
- Technical Documentation: Product specifications, safety documentation, and quality certificates can be provided subject to order and grade requirements.
- Strategic Sourcing Value: A versatile, high-demand industrial chemical suitable for manufacturers seeking dependable quality, scalable supply, and competitive procurement.
5. Commercial & Supply Information
- Minimum Order Quantity (MOQ): BULK 20 MT
- Loading Capacity: Approximately 20–25 MT per 20-foot container, subject to packaging configuration, product density, applicable transport regulations, and loading requirements
- Supply: Bulk international B2B supply available subject to specification, destination, and commercial terms

Reviews
There are no reviews yet.