
1. Product Overview
Yeast Extract Powder 70% Protein is a high-protein functional ingredient produced from yeast and designed for demanding food, feed, fermentation, and biotechnology applications. Its concentrated protein content and nutrient profile support microbial growth, nutritional enrichment, flavor development, and formulation performance. The powder offers industrial buyers a versatile, efficient ingredient for consistent large-scale production and specialized processing. Its broad application range makes it a strategically valuable component for manufacturers seeking dependable nutritional and functional raw materials.
2. Key Specifications & Technical Characteristics
- Product: Yeast Extract Powder
- Protein Content: 70%
- Grade: Industrial / Food & Feed applications, subject to specification
- Form: Fine powder
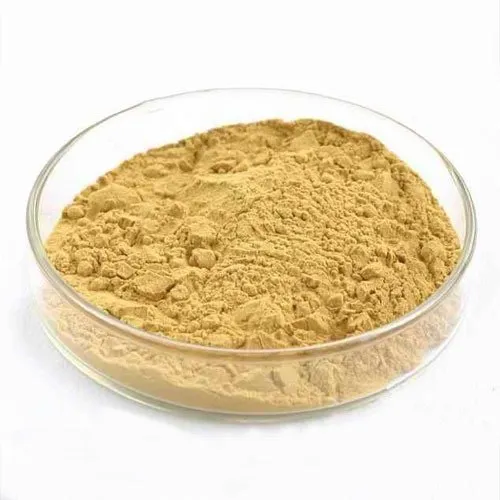
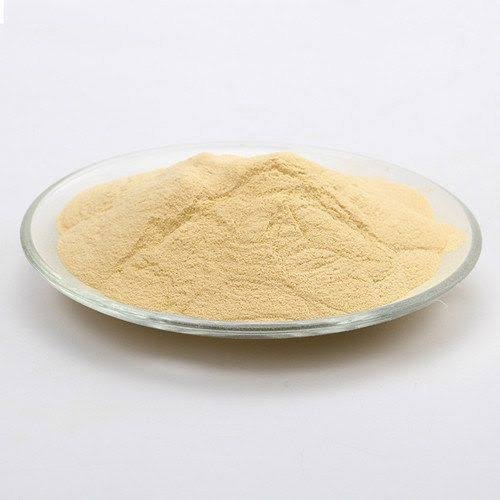
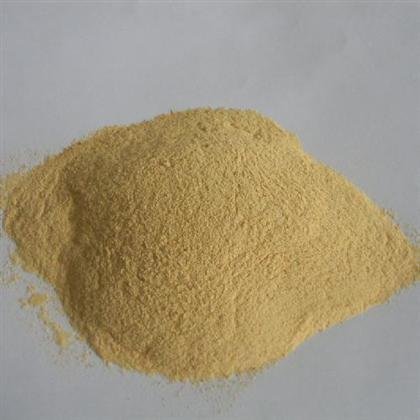
- Appearance: Typically light to medium yellowish-brown
- Composition: Concentrated yeast-derived proteins, peptides, amino acids, vitamins, minerals, and other soluble yeast nutrients
- Packaging: 25kg bags
- Shelf Life: Typically 24 months when stored under recommended conditions
- Storage: Keep sealed in a cool, dry, well-ventilated environment away from moisture and direct sunlight
- Origin: Available according to supplier and production batch
- Documentation: Product specification, Certificate of Analysis (COA), and relevant quality documentation available upon request
3. Core Industrial Applications
- Food Manufacturing: Used as a nutritional ingredient, flavor enhancer, and formulation component in processed foods, savory products, sauces, seasonings, and prepared foods.
- Animal Feed: Supports protein enrichment and nutritional formulation in feed products and premixes.
- Fermentation & Biotechnology: Provides readily available nutrients, amino acids, peptides, and growth factors for microbial and fermentation processes.
- Nutraceutical & Functional Formulations: Used as a concentrated source of yeast-derived protein and nutrients where formulation specifications permit.
- Industrial Processing: Its soluble nutrient profile supports efficient incorporation into large-scale formulations and controlled production systems.
4. Competitive Advantages
- High Protein Concentration: 70% protein provides efficient nutritional enrichment and formulation value.
- Consistent Quality: Designed for standardized industrial processing and repeatable batch performance.
- Supply Reliability: Suitable for bulk procurement and ongoing B2B supply programs.
- Logistics Capability: 25kg bag packaging supports practical handling, storage, palletization, and international shipment.
- Price Competitiveness: Bulk sourcing can support cost-efficient procurement for manufacturers and distributors.
- Technical Documentation: COA and product specifications can be provided to support quality control and purchasing requirements.
- Versatile Functionality: Combines nutritional and functional properties across food, feed, fermentation, and biotechnology applications.
5. Commercial & Supply Information
- Minimum Order Quantity (MOQ): BULK 20MT
- Loading Capacity: Approximately 20–25 MT per 20ft container, subject to packaging configuration and applicable shipping limits
- Packaging: 25kg bags
- Supply: Bulk and contract supply available for qualified B2B buyers
Reviews
There are no reviews yet.