
1. Product Overview
Sorbic Acid 99% is a high-purity organic preservative widely used to inhibit the growth of moulds, yeasts, and selected microorganisms across food, beverage, pharmaceutical, and industrial applications. Its strong preservation performance and broad formulation compatibility make it a dependable choice for manufacturers requiring consistent product stability and extended shelf life. Supplied at 99% purity, it supports precise formulation control and reliable batch-to-batch performance. The 25kg bag format is well suited to commercial manufacturing, distribution, and bulk ingredient procurement.
2. Key Specifications & Technical Characteristics
- Chemical composition: Sorbic Acid (C₆H₈O₂)
- Purity: ≥99%
- Grade: High-purity industrial/commercial grade
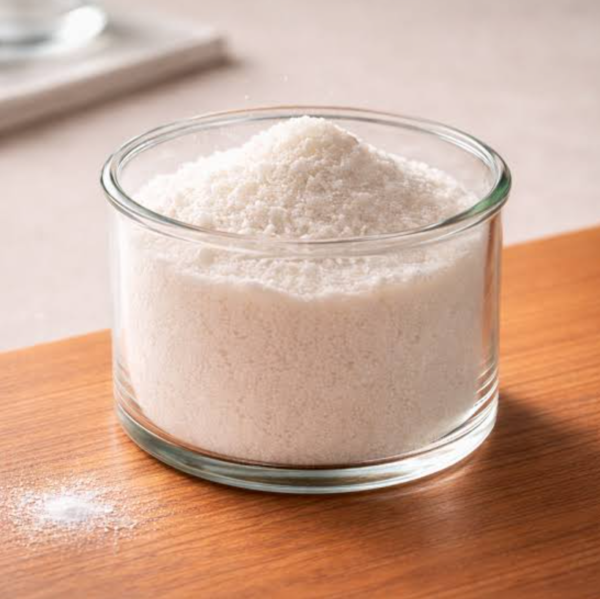
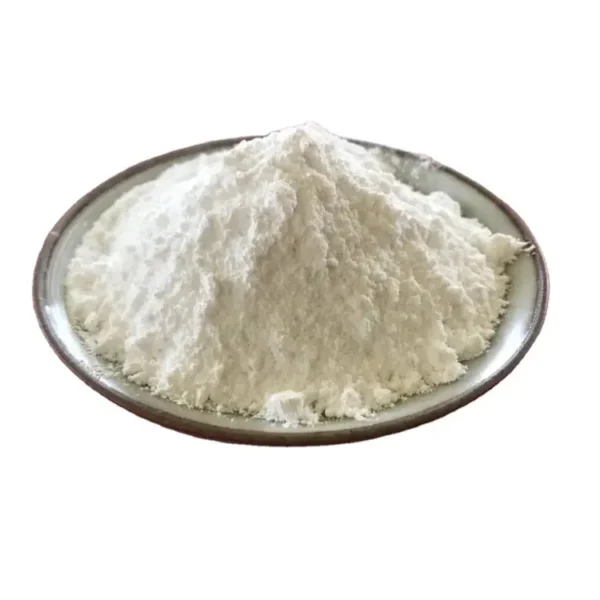
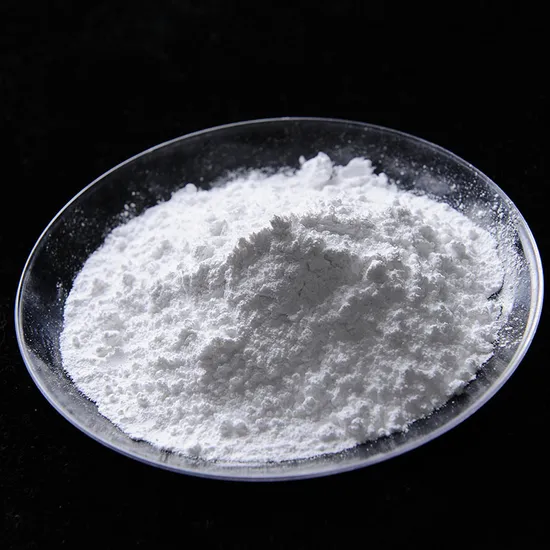
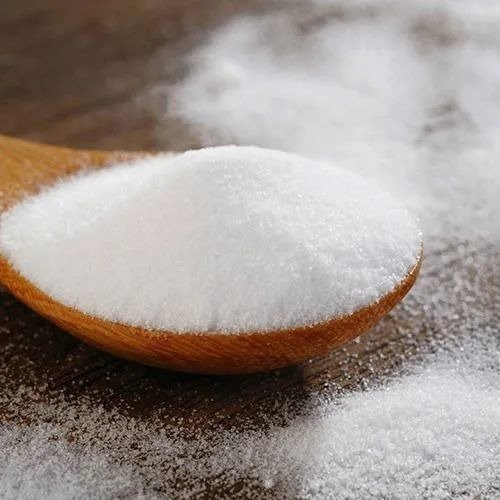
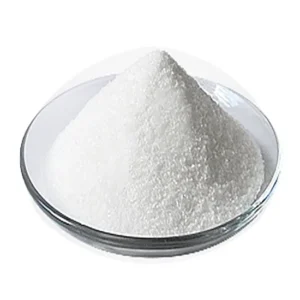
- Physical form: White crystalline powder or granules
- Function: Antimicrobial preservative and shelf-life stabilizer
- Solubility: Limited in water; suitable for controlled formulation and processing systems
- Packaging: 25kg industrial bag
- Shelf life: Typically 24 months when stored in sealed, dry conditions
- Storage: Cool, dry, well-ventilated environment away from moisture and direct sunlight
- Origin: Subject to supplier availability and batch specification
3. Core Industrial Applications
- Food & Beverage: Preservation of bakery products, sauces, beverages, dairy-related products, confectionery, and other formulations susceptible to mould and yeast growth.
- Pharmaceuticals: Used as a preservative ingredient in selected pharmaceutical and topical formulations where applicable.
- Personal Care: Supports microbial control in selected cosmetic and personal-care formulations.
- Industrial Formulations: Used where controlled antimicrobial preservation is required.
- Performance Advantage: Provides effective preservation at controlled concentrations, helping manufacturers maintain product quality and reduce spoilage-related losses.
4. Competitive Advantages
- High Purity: 99% specification supports dependable formulation accuracy and consistent processing.
- Quality Consistency: Suitable for applications requiring controlled and repeatable preservative performance.
- Supply Reliability: Commercial 25kg packaging supports efficient inventory planning and repeat procurement.
- Logistics Capability: Standardized industrial packaging facilitates handling, storage, palletization, and international shipment.
- Cost Efficiency: High-purity material can support efficient dosage control and optimized formulation economics.
- Technical Documentation: Product specifications, certificates, and supporting documentation can be provided subject to order and supplier availability.
- Strategic Sourcing: A practical ingredient choice for manufacturers seeking reliable preservative performance, scalable supply, and consistent commercial specifications.
5. Commercial & Supply Information
- Minimum Order Quantity (MOQ): BULK 20MT
- Loading Capacity: Subject to container type, packaging configuration, and applicable shipping requirements
- Packaging: 25kg bags
- Supply: Bulk commercial and international supply available

Reviews
There are no reviews yet.