
1. Product Overview
Potassium Citrate 99% is a high-purity potassium salt of citric acid supplied in convenient 25kg bags for industrial and commercial applications. It is widely used as a buffering agent, acidity regulator, stabilizer, and potassium source across food, beverage, pharmaceutical, and specialty chemical formulations. Its high purity and consistent composition support reliable processing, formulation accuracy, and finished-product quality. As a versatile multifunctional ingredient, it is strategically important for manufacturers seeking dependable performance and efficient bulk sourcing.
2. Key Specifications & Technical Characteristics
- Chemical Composition: Potassium citrate; commonly supplied as tripotassium citrate
- Purity: ≥99%
- Grade: Industrial/commercial grade; food or pharmaceutical grade subject to applicable specification and certification
- CAS Number: 866-84-2
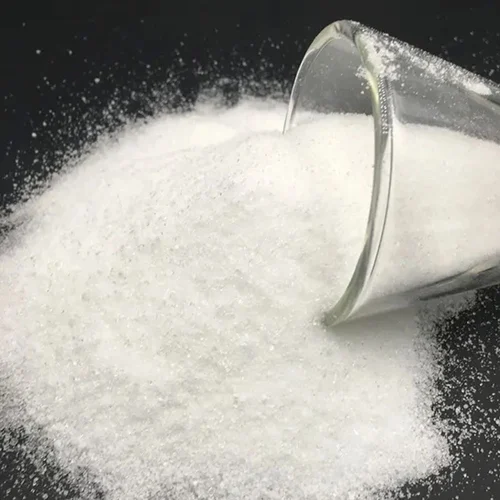
- Physical Form: White crystalline powder or granules
- Solubility: Highly soluble in water
- Function: Buffering agent, acidity regulator, stabilizer, potassium source
- Packaging: 25kg bags; bulk packaging available subject to order requirements
- Shelf Life: Typically 24 months when stored correctly in original, sealed packaging
- Storage: Store in a cool, dry, well-ventilated area away from moisture and incompatible materials
- Origin: Available from international supply sources; origin confirmed according to shipment and batch documentation
3. Core Industrial Applications
- Food & Beverage: Used as an acidity regulator, buffering agent, stabilizer, and mineral source in beverages, processed foods, confectionery, and formulated products.
- Pharmaceutical Manufacturing: Used in formulations where controlled alkalinity and potassium supplementation are required, subject to applicable pharmaceutical specifications.
- Nutraceuticals & Supplements: Provides a readily available potassium source for mineral and electrolyte formulations.
- Chemical Processing: Functions as a buffering and formulation component in specialty chemical applications.
- Industrial Formulations: Supports pH control, formulation stability, and consistent processing performance.
Its high purity, water solubility, and predictable chemical characteristics make it suitable for applications requiring controlled formulation performance and repeatable batch quality.
4. Competitive Advantages
- High Purity: 99% specification supports consistent formulation and processing performance.
- Quality Consistency: Controlled composition helps manufacturers maintain reliable batch-to-batch results.
- Supply Reliability: Structured bulk sourcing supports recurring industrial procurement requirements.
- Logistics Capability: 25kg bags facilitate warehouse handling, palletization, and international shipment consolidation.
- Price Competitiveness: Bulk procurement can support improved cost efficiency for regular-volume buyers.
- Sustainability: Efficient bulk packaging and consolidated shipment planning can help reduce unnecessary packaging and transportation intensity.
- Technical Documentation: Product specifications, certificates of analysis, safety documentation, and other compliance documents can be provided subject to grade and supplier availability.
5. Commercial & Supply Information
- Packaging: 25kg bag
- Minimum Order Quantity (MOQ): BULK 20MT
- Loading Capacity: Approximately 20–22 MT per 20ft container, depending on packaging configuration, palletization, and applicable shipping restrictions
- Supply: Available for bulk international B2B orders
- Documentation: Commercial and technical documentation available subject to order and grade requirements


Reviews
There are no reviews yet.