
1. Product Overview
Vital Wheat Gluten Food Grade is a high-protein wheat-derived ingredient designed to improve dough strength, elasticity, structure, and water absorption in food manufacturing. It is widely used in bakery, pasta, meat-alternative, and processed food applications where consistent protein functionality is essential. Its strong binding and texturizing performance helps manufacturers optimize product quality, processing efficiency, and formulation consistency. Supplied in 25kg bags, it provides a practical format for commercial and industrial food production.
2. Key Specifications & Technical Characteristics
- Material Composition: Concentrated wheat protein derived from wheat flour.
- Grade: Food Grade.
- Protein Content: Typically high-protein, subject to supplier specification and applicable food-grade standards.
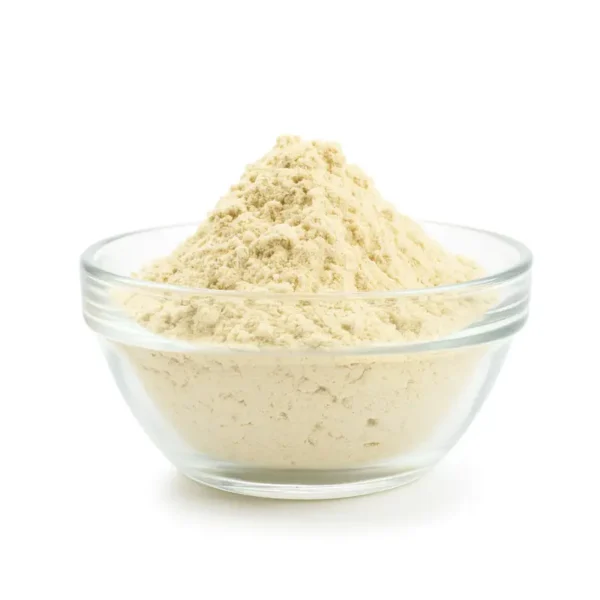
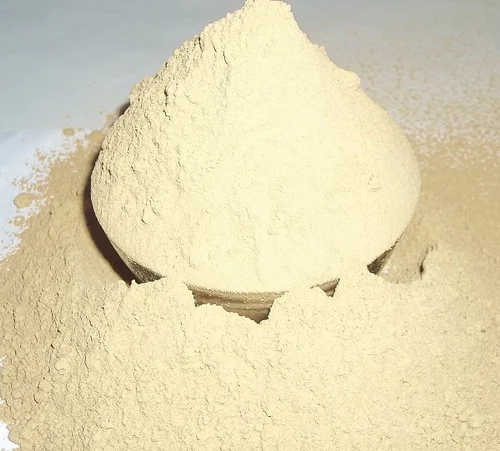
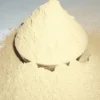
- Physical Form: Fine, free-flowing powder.
- Colour: Cream to light beige.
- Functional Characteristics: High water absorption, dough-strengthening, elasticizing, binding, and texturizing properties.
- Gluten Functionality: Supports dough development, volume, chewiness, and structural stability.
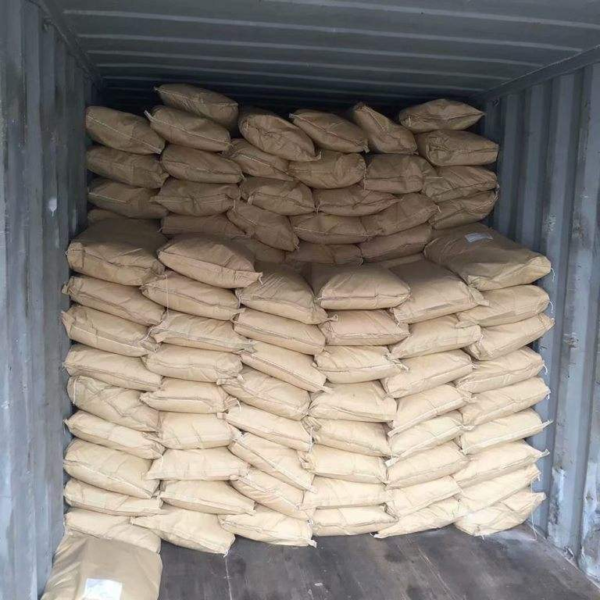
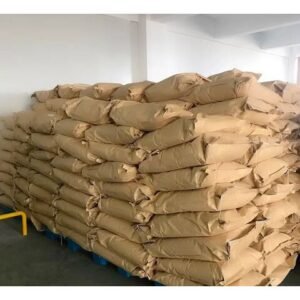
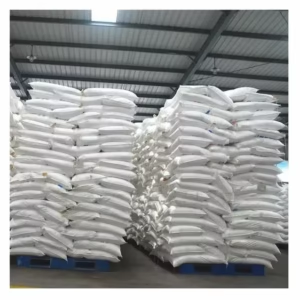
- Packaging: 25kg industrial-grade bags.
- Shelf Life: Typically 12–24 months when stored unopened under recommended dry, cool, and hygienic conditions.
- Storage: Protect from moisture, heat, contamination, and direct sunlight; maintain in a dry, well-ventilated storage environment.
3. Core Industrial Applications
- Bakery Products: Enhances dough strength, elasticity, volume, texture, and processing tolerance in bread, rolls, pizza bases, and other baked goods.
- Pasta & Noodles: Improves protein structure, firmness, elasticity, and cooking performance.
- Meat Alternatives: Provides binding, chewiness, structure, and protein enrichment in plant-based formulations.
- Food Manufacturing: Used as a functional protein ingredient in formulated foods requiring improved texture and structural stability.
- Protein-Enriched Products: Supports higher-protein formulations while maintaining desirable processing and eating characteristics.
- Processing Advantage: Its concentrated protein functionality can improve formulation efficiency compared with lower-protein wheat ingredients.
4. Competitive Advantages
- Quality Consistency: Consistent functional performance supports repeatable production and formulation control.
- Supply Reliability: Suitable for planned bulk procurement and ongoing industrial supply programs.
- Logistics Capability: 25kg packaging facilitates handling, warehousing, palletization, and international shipment.
- Price Competitiveness: Bulk sourcing supports commercially efficient procurement for manufacturers and distributors.
- Functional Performance: High protein functionality delivers effective dough strengthening, binding, elasticity, and textural improvement.
- Sustainability: Wheat-based protein supports efficient utilization of agricultural raw materials within food production systems.
- Technical Documentation: Product specifications, quality documentation, and relevant food-safety information can be provided subject to supplier requirements.
5. Commercial & Supply Information
- Minimum Order Quantity (MOQ): BULK 20MT
- Loading Capacity: Container loading capacity depends on packaging configuration, palletization, container type, and applicable weight limits.
- Packaging: 25kg bags
- Supply Format: Bulk commercial and industrial supply
- Target Buyers: Food manufacturers, ingredient distributors, bakeries, pasta manufacturers, plant-based food producers, and international wholesalers.
Reviews
There are no reviews yet.