
1. Product Overview
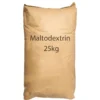
Maltodextrin Food Grade is a purified, easily digestible carbohydrate derived from starch and supplied as a fine, white powder for food and industrial processing applications. It is widely used as a bulking agent, carrier, texture modifier, stabilizer, and energy source across food, beverage, dairy, confectionery, and nutritional formulations. Its neutral profile, high process compatibility, and reliable dispersibility support consistent formulation and efficient large-scale production. The 25kg bag format provides a practical solution for commercial manufacturers requiring dependable bulk ingredient supply.
2. Key Specifications & Technical Characteristics
- Material: Food-grade maltodextrin derived from starch
- Composition: Glucose polymers produced through controlled starch hydrolysis
- Grade: Food Grade
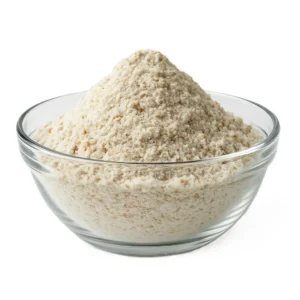
- Form: Fine, free-flowing powder
- Colour: White to off-white
- Taste/Odor: Mild to neutral
- Solubility: Readily soluble in water
- Functional properties: Bulking, carrier, texture modification, stabilization, and controlled sweetness
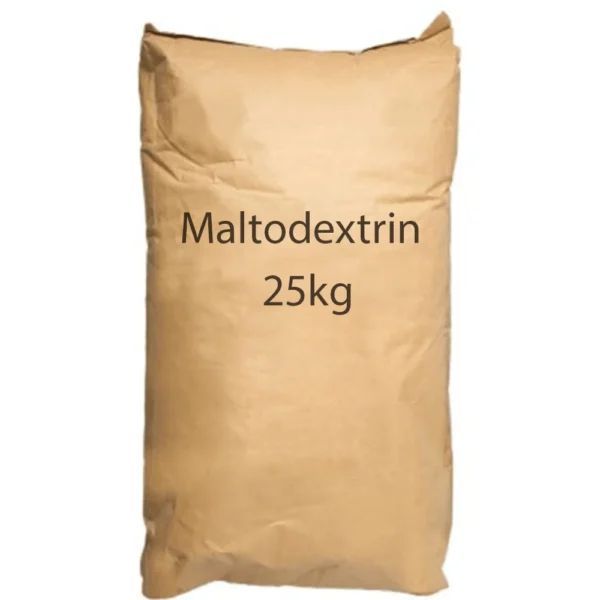
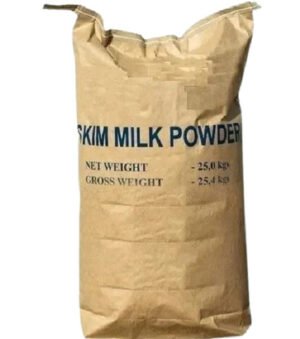
- Packaging: 25kg bags; bulk packaging available subject to specification and order requirements
- Shelf Life: Typically up to 24 months when stored in cool, dry conditions in sealed original packaging
- Storage: Protect from moisture, direct sunlight, and excessive heat; maintain in a dry, well-ventilated storage environment
3. Core Industrial Applications
- Food Manufacturing: Used in sauces, instant foods, processed foods, bakery products, and dry mixes as a bulking and texture-modifying ingredient.
- Beverages: Supports powdered drink formulations, instant beverages, and nutritional products as a carrier and solids contributor.
- Confectionery: Helps improve texture, body, stability, and processing characteristics in sweets and confectionery formulations.
- Dairy & Nutrition: Used in dairy powders, meal replacements, sports nutrition, and carbohydrate-based nutritional formulations.
- Encapsulation & Flavour Systems: Functions as an effective carrier for flavours, colours, oils, and other sensitive ingredients.
- Industrial Efficiency: Its free-flowing form, water solubility, and broad formulation compatibility support efficient mixing, processing, and consistent finished-product quality.
4. Competitive Advantages
- Quality Consistency: Controlled food-grade production supports dependable performance across production batches.
- Supply Reliability: Suitable for recurring commercial procurement and large-volume manufacturing requirements.
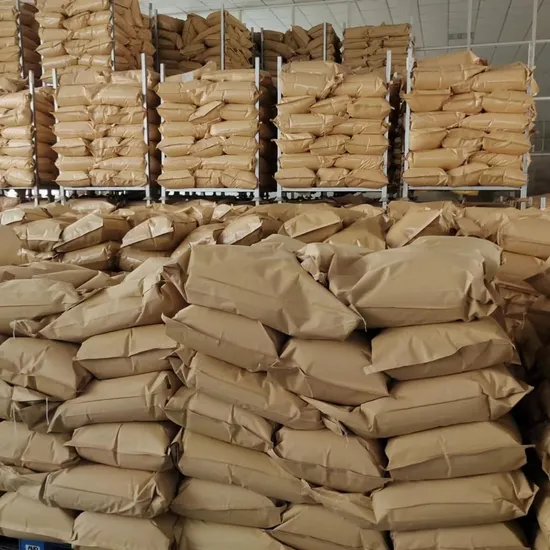
- Logistics Capability: Standardized 25kg packaging facilitates handling, warehousing, palletization, and international shipment.
- Price Competitiveness: Bulk procurement enables manufacturers and distributors to optimize ingredient costs and supply planning.
- Versatile Performance: Provides multiple functional benefits within a wide range of food, beverage, nutritional, and industrial formulations.
- Documentation: Product specifications, quality documentation, and relevant compliance information can be provided subject to buyer and market requirements.
- Sourcing Value: A practical ingredient choice for manufacturers seeking consistent quality, scalable supply, and efficient bulk procurement.
5. Commercial & Supply Information
- Minimum Order Quantity (MOQ): BULK 20MT
- Packaging: 25kg bags
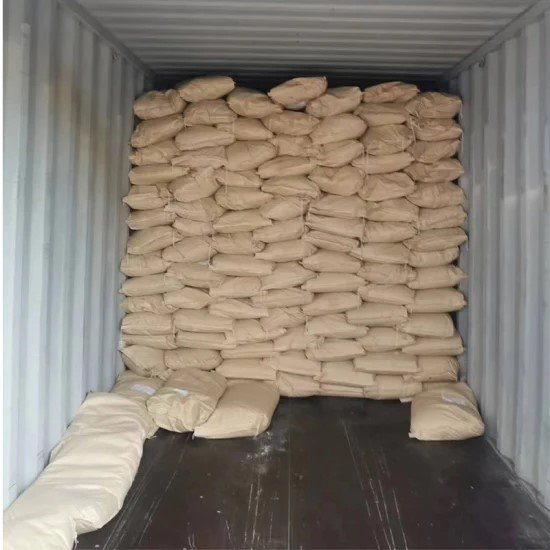
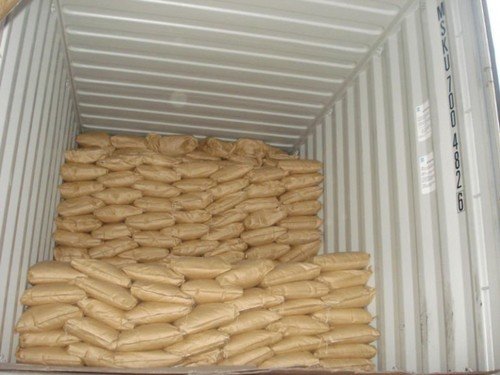
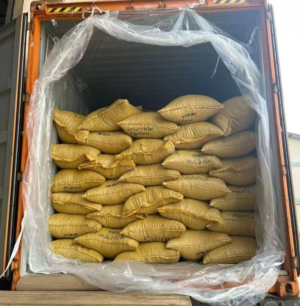
- Loading Capacity: Approximately 20–25 MT per 20-foot container, subject to packaging configuration, palletization, and applicable shipping requirements
- Supply: Bulk commercial and international supply available
Reviews
There are no reviews yet.