
1. Product Overview
Extra Virgin Olive Oil Food Grade is a premium edible oil mechanically extracted from high-quality olives without chemical refining, offering natural flavor, aroma, and nutritional value. It is widely used across food processing, culinary manufacturing, sauces, dressings, prepared foods, and premium foodservice applications. Its combination of quality, versatility, and recognized consumer demand makes it a strategically important ingredient for food manufacturers and bulk buyers. Consistent quality and scalable bulk supply support reliable procurement for international B2B operations.
2. Key Specifications & Technical Characteristics
- Product: Extra Virgin Olive Oil Food Grade
- Grade: Food Grade / Extra Virgin
- Composition: Predominantly natural olive oil triglycerides, with naturally occurring minor components including polyphenols, tocopherols, and other olive-derived compounds
- Purity: 100% olive oil, subject to applicable extra-virgin quality standards
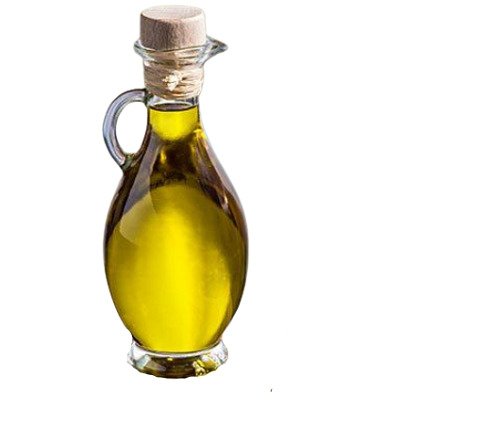
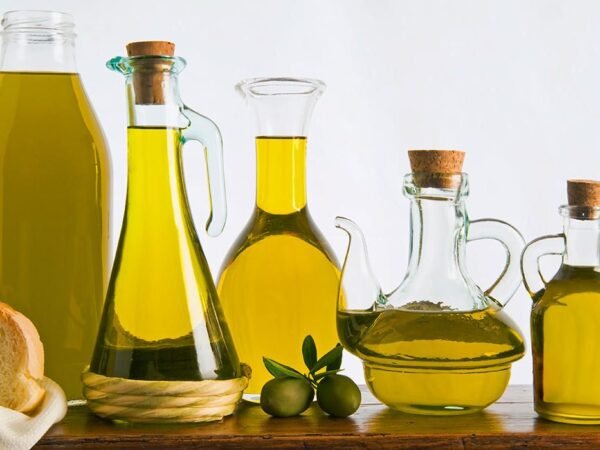
- Appearance: Clear to slightly hazy liquid
- Color: Green to golden-yellow, depending on olive variety, harvest, and processing
- Flavor & Aroma: Characteristic fresh olive profile; may range from mild and fruity to robust and peppery
- Free Fatty Acidity: Typically ≤0.8% oleic acid for extra virgin classification, subject to applicable standards and batch testing
- Packaging Options: Bulk tanker, flexitank, IBC, drums, or other export packaging according to buyer requirements
- Storage: Store in a cool, dry environment away from direct sunlight, heat, oxygen, and strong odors
- Shelf Life: Typically 18–24 months when properly packaged and stored, subject to producer specification
3. Core Industrial Applications
- Food Manufacturing: Used in sauces, marinades, dressings, spreads, ready-to-eat meals, and premium processed foods.
- Bakery & Culinary Production: Suitable for baking, cooking, frying applications where appropriate, and specialty food formulations.
- Foodservice & Hospitality: Supplied in bulk for restaurants, catering companies, hotels, and institutional kitchens.
- Premium Packaged Foods: Used as a value-added ingredient where natural origin, flavor profile, and premium positioning are commercially important.
- Specialty Food Processing: Suitable for formulations requiring a high-quality plant-based edible oil with distinctive sensory characteristics.
4. Competitive Advantages
- Quality Consistency: Controlled sourcing and quality assessment support dependable specifications across commercial batches.
- Supply Reliability: Bulk procurement options facilitate stable supply for manufacturers, distributors, and international buyers.
- Logistics Capability: Export-oriented packaging and bulk-loading options support efficient international transportation and scalable purchasing.
- Price Competitiveness: Bulk 20 MT procurement provides opportunities for optimized landed cost and improved purchasing efficiency.
- Product Integrity: Food-grade handling and appropriate packaging help protect oil quality throughout storage and transportation.
- Sustainability: Plant-based origin and mechanical extraction support a naturally derived ingredient suitable for sustainability-conscious food supply chains.
- Documentation & Technical Support: Commercial buyers can be supported with relevant product specifications, certificates of analysis, quality documentation, and export documentation as applicable.
5. Commercial & Supply Information
- Minimum Order Quantity (MOQ): BULK 20 MT
- Loading Capacity: Up to approximately 20 MT per container, depending on packaging configuration, container type, and applicable transport weight limits
Reviews
There are no reviews yet.