
1. Product Overview
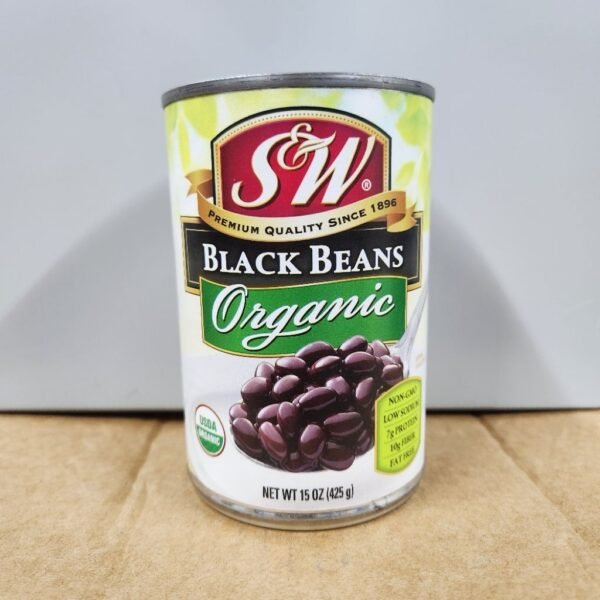
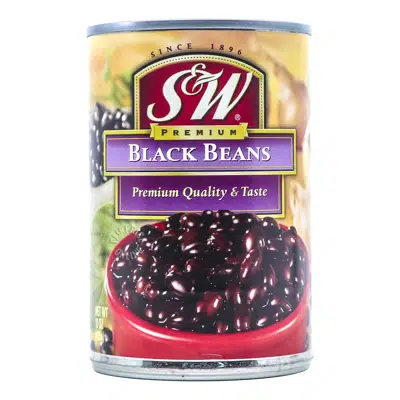
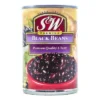
S&W Premium Black Beans — 425g are premium-quality canned black beans selected for consistent size, color, texture, and dependable culinary performance. They are primarily used by foodservice operators, food manufacturers, distributors, retailers, and institutional buyers requiring convenient, ready-to-use legumes. The product delivers efficient preparation, extended shelf stability, and consistent quality, reducing processing time and handling requirements. Its standardized retail-ready format supports reliable sourcing across foodservice, wholesale, and international distribution channels.
2. Key Specifications & Technical Characteristics
- Product: S&W Premium Black Beans
- Net Weight: 425g per can
- Product Type: Canned black beans
- Grade: Premium food grade
- Main Material: Whole black beans with canning liquid
- Form: Whole cooked beans
- Color: Characteristic deep black to dark purple
- Texture: Tender, firm, and suitable for food preparation
- Processing: Cooked and commercially canned for convenient use and extended shelf stability
- Packaging: 425g cans; outer carton configurations available according to supply requirements
- Shelf Life: Typically extended under unopened, properly stored conditions; exact shelf life should be confirmed from the product lot and supplier documentation
- Storage: Store in a cool, dry place away from direct sunlight; refrigerate after opening
- Origin: Subject to available production batch and supplier documentation
3. Core Industrial Applications
- Foodservice & Catering: Ready-to-use ingredient for restaurants, hotels, caterers, and institutional kitchens.
- Food Manufacturing: Suitable for incorporation into prepared meals, bean-based products, soups, sauces, salads, and other processed foods.
- Retail & Wholesale Distribution: Convenient canned format supports supermarkets, wholesalers, grocery distributors, and international food traders.
- Mexican, Latin American & Global Cuisine: Commonly used in burritos, tacos, rice-and-bean dishes, salads, stews, and side dishes.
- Operational Efficiency: Pre-cooked and canned beans reduce soaking, cooking, labor, water, and preparation time compared with dried alternatives.
- Consistency: Standardized portions and controlled processing provide dependable texture and performance across commercial food applications.
4. Competitive Advantages
- Quality Consistency: Premium-grade black beans with controlled processing for dependable appearance, texture, and culinary performance.
- Supply Reliability: Established branded product suitable for structured wholesale procurement and recurring commercial requirements.
- Logistics Capability: Shelf-stable canned packaging supports efficient warehousing, containerized transport, and international distribution.
- Price Competitiveness: Ready-to-use format can reduce preparation labor and associated processing costs for commercial buyers.
- Extended Shelf Stability: Commercial canning enables long-term storage when unopened and properly handled.
- Market Versatility: Suitable across retail, foodservice, catering, manufacturing, and wholesale distribution channels.
- Documentation: Product specifications, batch information, and commercial documentation can be provided subject to supplier availability.
5. Commercial & Supply Information
- Minimum Order Quantity (MOQ): BULK 20MT
- Loading Capacity: Subject to container type, packaging configuration, palletization, and applicable weight restrictions
- Supply Format: Bulk commercial supply for wholesale, foodservice, distribution, and international procurement
Reviews
There are no reviews yet.