
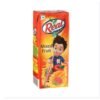
1. Product Overview
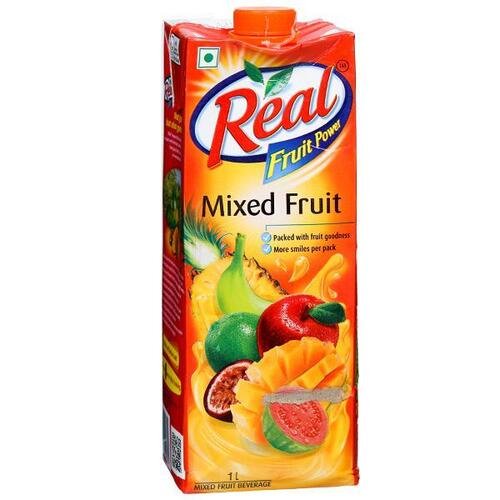
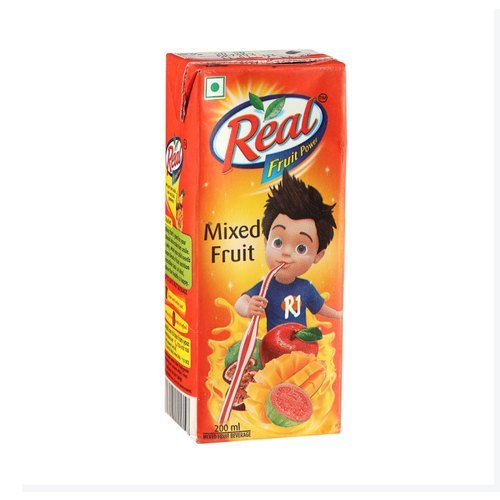
Real Mixed Fruit Juice – 200 ml is a convenient ready-to-drink fruit beverage formulated to deliver a refreshing mixed-fruit taste in a practical single-serve format. It is suitable for beverage distributors, retailers, hospitality operators, catering businesses, schools, offices, and foodservice channels. The 200 ml pack supports convenient portion control, easy handling, and fast retail turnover. Its broad consumer appeal makes it a commercially attractive addition to beverage portfolios seeking accessible, ready-to-consume fruit drinks.
2. Key Specifications & Technical Characteristics
- Product Type: Ready-to-drink mixed fruit juice beverage
- Composition: Mixed fruit juice/fruit preparations, water, and permitted beverage ingredients
- Grade: Food Grade
- Form: Liquid
- Appearance: Fruit-coloured, homogeneous beverage
- Taste & Aroma: Refreshing mixed-fruit flavour with characteristic fruity aroma
- Packaging: 200 ml individual retail packs
- Shelf Life: Typically 6–12 months when unopened and stored under recommended conditions; confirm manufacturer specification
- Storage: Store in a cool, dry place away from direct sunlight; refrigerate after opening where applicable
- Origin: Subject to supplier/manufacturer availability
- Documentation: Product specifications, packaging details, and applicable food-safety documentation available upon request
3. Core Industrial Applications
- Retail & Wholesale Distribution: Suitable for supermarkets, convenience stores, beverage wholesalers, and general retail channels.
- Foodservice & Hospitality: Practical for hotels, restaurants, cafés, catering companies, and institutional foodservice.
- Schools & Workplace Catering: The single-serve format supports convenient portion distribution and controlled serving sizes.
- Events & Hospitality Supply: Compact packaging enables efficient distribution at meetings, events, conferences, and catered functions.
- Vending & Convenience Channels: Ready-to-drink presentation supports fast consumption and efficient merchandising.
The compact 200 ml format offers advantages in portability, portion control, storage efficiency, and consumer convenience compared with larger-format beverages.
4. Competitive Advantages
- Consistent Quality: Standardized formulation and single-serve presentation support reliable product quality across commercial orders.
- Supply Reliability: Suitable for structured wholesale procurement and recurring beverage distribution programs.
- Logistics Efficiency: Compact 200 ml packaging facilitates handling, palletization, transportation, and retail distribution.
- Commercial Competitiveness: Bulk procurement can support competitive landed costs and attractive resale margins.
- Market Versatility: Broad suitability across retail, hospitality, catering, institutional, and convenience channels.
- Sustainability Consideration: Efficient single-serve packaging can support practical transport and storage optimization.
- Documentation Support: Product specifications and relevant commercial documentation can be provided according to supply requirements.
5. Commercial & Supply Information
- Minimum Order Quantity (MOQ): BULK 20MT
- Loading Capacity: Subject to packaging configuration, palletization, container type, and final shipment specifications.
Reviews
There are no reviews yet.