
1. Product Overview
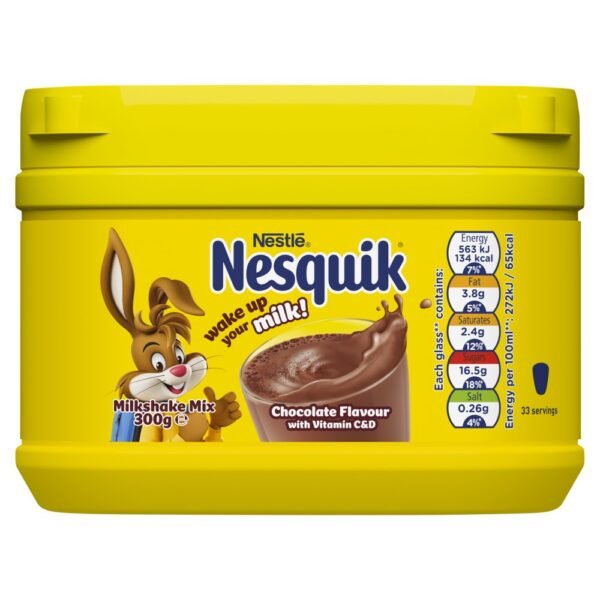
Nesquik Chocolate Milk – 300 ml is a ready-to-drink chocolate-flavoured milk beverage formulated to deliver a smooth, creamy texture and familiar chocolate taste in a convenient single-serve format. It is suited to wholesale distribution, retail, foodservice, vending, convenience channels, and institutional supply. Its combination of established consumer appeal, portion convenience, and easy handling makes it a commercially attractive beverage for high-volume procurement. The product supports efficient sourcing for distributors seeking recognizable, ready-to-market chocolate milk beverages.
2. Key Specifications & Technical Characteristics
- Product Type: Ready-to-drink chocolate milk beverage
- Flavour: Chocolate
- Net Volume: 300 ml per unit
- Composition: Milk and dairy ingredients, water, sugar/sweetening ingredients, cocoa/chocolate flavouring, and permitted stabilising or processing ingredients as applicable to the specific formulation
- Physical Characteristics: Smooth, homogeneous liquid with a chocolate-brown colour and creamy chocolate flavour
- Grade: Consumer food/beverage grade
- Packaging: 300 ml single-serve retail packaging; secondary and bulk cartons available subject to supplier configuration
- Shelf Life: Typically subject to manufacturer batch specification and storage conditions
- Storage: Store according to the manufacturer’s stated temperature and handling requirements
- Origin: Manufacturer-specific; confirmed according to the supplied batch and commercial documentation
3. Core Industrial Applications
- Retail & Wholesale Distribution: Suitable for supermarkets, convenience stores, beverage distributors, and wholesale channels.
- Foodservice & Hospitality: Convenient single-serve beverage option for cafés, restaurants, hotels, catering operations, and institutional foodservice.
- Vending & Grab-and-Go: Compact 300 ml format supports portion-controlled beverage sales and convenient consumption.
- Schools & Institutional Supply: Suitable for approved foodservice and institutional beverage programmes where chocolate milk products are permitted.
- Commercial Resale: Recognizable product positioning can support faster market acceptance compared with lesser-known alternatives.
4. Competitive Advantages
- Recognizable Product Positioning: Established chocolate-milk positioning provides strong consumer familiarity and commercial appeal.
- Consistent Quality: Manufactured to defined food and beverage quality specifications, supporting dependable wholesale supply.
- Convenient Format: 300 ml single-serve packaging is practical for retail, vending, foodservice, and on-the-go consumption.
- Supply & Logistics Efficiency: Cartonized retail units facilitate storage, handling, palletisation, and international wholesale distribution.
- Commercial Competitiveness: Bulk procurement can support competitive unit economics for distributors and high-volume buyers.
- Documentation Support: Product specifications, batch information, packaging details, and relevant commercial documentation can be provided subject to supplier availability.
5. Commercial & Supply Information
- Minimum Order Quantity (MOQ): BULK 20MT
- Loading Capacity: Subject to packaging configuration, palletisation, container type, and destination requirements; final loading capacity to be confirmed at quotation stage.
Reviews
There are no reviews yet.