
- Product Overview
Silicon Dioxide (SiO₂) is a high-performance inorganic mineral widely used as a functional ingredient, reinforcing agent, filler, and processing aid across multiple industrial sectors. It is valued for its chemical stability, high surface area, moisture absorption, and excellent dispersion characteristics. The product supports improved formulation performance, product consistency, durability, and processing efficiency in demanding manufacturing environments. As a strategically important industrial material, Silicon Dioxide serves diverse applications across chemicals, food processing, pharmaceuticals, coatings, rubber, plastics, and construction. - Key Specifications & Technical Characteristics
- Chemical Composition: Silicon Dioxide (SiO₂)
- Purity: Industrial and application-specific grades available
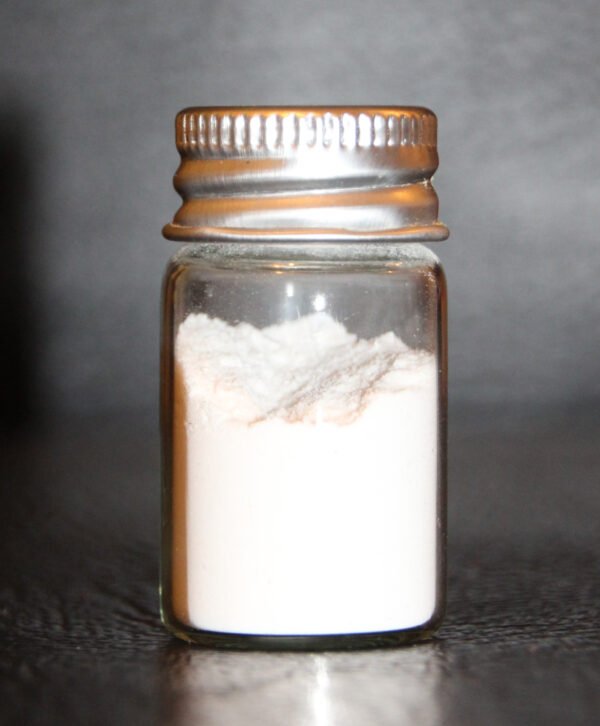
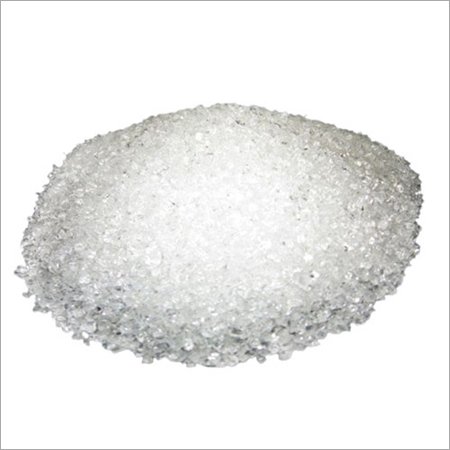
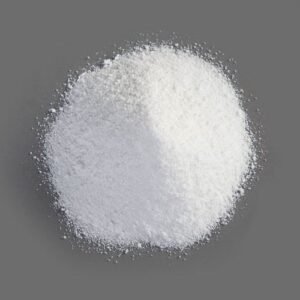
- Form: Fine powder
- Color: White to off-white
- Particle Size: Fine, controlled particle-size distribution according to application requirements
- Physical Characteristics: High chemical stability, high surface area, excellent absorption and dispersion properties
- Packaging Options: 25kg bags, jumbo bags, and bulk packaging
- Shelf Life: Typically 24 months when stored in dry, sealed conditions
- Storage: Keep sealed and protected from moisture, contamination, and excessive humidity
- Origin: Available from qualified international supply sources
- Core Industrial Applications
- Food & Beverage: Used as an anti-caking and flow-control agent in selected food applications.
- Pharmaceuticals: Utilized as an excipient, carrier, and processing aid where compliant grades are required.
- Rubber & Plastics: Functions as a reinforcing filler and performance-enhancing additive.
- Paints & Coatings: Supports rheology control, matting, reinforcement, and formulation stability.
- Construction Materials: Used in cementitious systems, specialty mortars, sealants, and high-performance formulations.
- Chemical Manufacturing: Applied as an absorbent, carrier, filler, and processing component.
- Animal Feed & Agriculture: Selected grades may be used for flow control and moisture management where permitted.
- Performance Advantage: Its chemical inertness, fine particle structure, absorption capacity, and consistent dispersion enable reliable formulation performance and efficient processing.
- Competitive Advantages
- Quality Consistency: Controlled specifications support dependable performance across production batches.
- Supply Reliability: Suitable for recurring industrial procurement and bulk-volume requirements.
- Logistics Capability: Available in industrial packaging formats designed for efficient handling, storage, and international shipment.
- Price Competitiveness: Bulk sourcing options support cost-effective procurement for commercial-scale operations.
- Sustainability: Long service life and multifunctional performance can help optimize material efficiency in selected formulations.
- Technical Documentation: Product specifications, technical data, and application documentation can be provided according to grade and buyer requirements.
- Strategic Sourcing Value: Combines dependable quality, scalable supply, flexible packaging, and competitive commercial terms for industrial buyers.
- Commercial & Supply Information
- Minimum Order Quantity (MOQ): BULK 20MT
- Loading Capacity: Approximately 20–25 MT per 20-foot container, subject to packaging configuration, product density, and applicable shipping restrictions.


Reviews
There are no reviews yet.