
- Product Overview
Dextrose Monohydrate is a high-purity crystalline glucose ingredient containing one molecule of water of crystallization, widely used as a readily available carbohydrate and sweetening agent. It is primarily supplied to the food, beverage, pharmaceutical, fermentation, and animal nutrition industries where consistent sweetness, energy value, and functional performance are essential. Its excellent solubility, rapid energy availability, and reliable batch consistency make it a versatile alternative to other carbohydrate ingredients. As a globally traded industrial raw material, Dextrose Monohydrate supports efficient formulation, processing, and large-scale manufacturing across multiple sectors. - Key Specifications & Technical Characteristics
- Chemical composition: D-Glucose monohydrate (C₆H₁₂O₆·H₂O)
- Grade: Food, pharmaceutical, fermentation, or feed grade subject to specification
- Purity: Typically ≥99% on a dry-solids basis, subject to grade and supplier specification
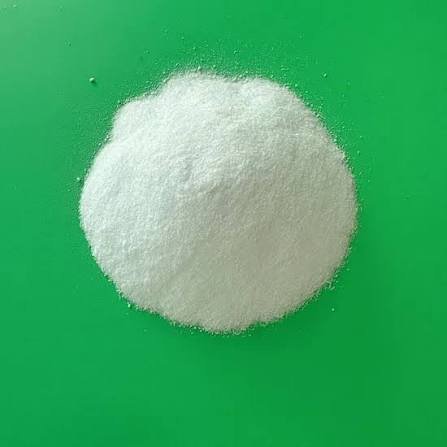
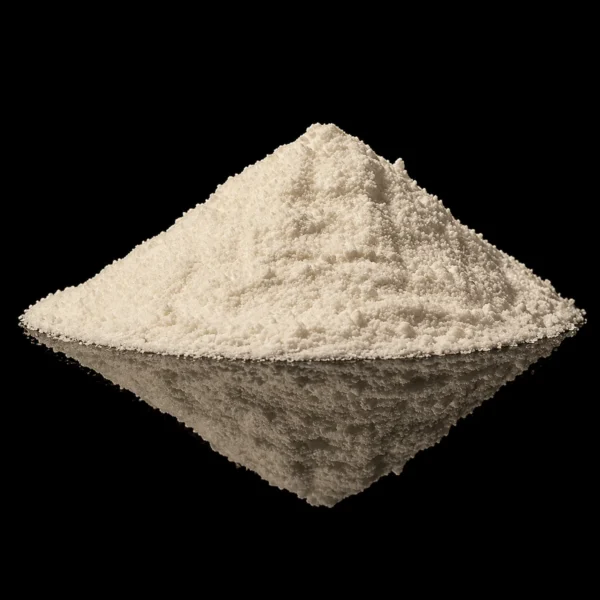
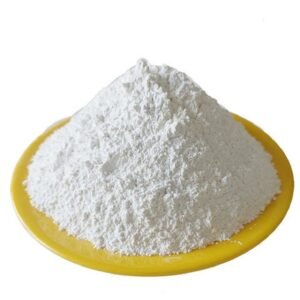
- Physical form: Free-flowing crystalline powder
- Color: White to off-white
- Solubility: Highly soluble in water
- Taste: Clean, characteristic sweet glucose profile
- Functional characteristics: Rapidly available carbohydrate, sweetener, bulking agent, and fermentation substrate
- Packaging options: 25kg bags and bulk industrial packaging available
- Shelf life: Typically 24 months when stored under recommended conditions
- Storage: Store in a cool, dry, well-ventilated environment in tightly sealed packaging
- Origin: Available from international production sources, subject to supply availability and buyer requirements
- Core Industrial Applications
- Food & Beverage: Used in confectionery, bakery products, dairy formulations, desserts, beverages, and processed foods as a sweetener and carbohydrate source.
- Pharmaceuticals: Used as an excipient and carbohydrate ingredient in oral and other pharmaceutical formulations where controlled quality and solubility are required.
- Fermentation: Serves as an efficient glucose substrate for fermentation processes, including biotechnology and industrial fermentation applications.
- Animal Nutrition: Provides a readily digestible energy source for selected feed and nutritional formulations.
- Industrial Processing: Used in formulations requiring high water solubility, consistent sweetness, and dependable carbohydrate performance.
- Performance advantages: Rapid dissolution, predictable functionality, consistent quality, and broad compatibility with industrial formulations can support efficient processing and formulation control.
- Competitive Advantages
- Quality consistency: Controlled crystalline structure, purity, and functional performance for dependable production outcomes.
- Supply reliability: Suitable for recurring industrial procurement and high-volume sourcing programs.
- Logistics capability: Available in standardized industrial packaging with bulk supply options to support international distribution.
- Price competitiveness: Efficient bulk procurement can help manufacturers optimize raw-material costs and supply-chain planning.
- Sustainability: A versatile carbohydrate ingredient that can support efficient formulation and resource-conscious manufacturing processes.
- Technical documentation: Product specifications, certificates of analysis, safety documentation, and quality information can be provided subject to grade and supply agreement.
- Strategic sourcing value: Combines broad industrial applicability, consistent performance, scalable supply, and commercial flexibility for professional buyers.
- Commercial & Supply Information
- Minimum Order Quantity (MOQ): BULK 20MT
- Loading Capacity: Subject to container type, packaging configuration, and applicable shipping requirements


Reviews
There are no reviews yet.