
1. Product Overview
Sodium Diacetate 99% is a high-purity organic acid salt used primarily as an antimicrobial, preservative, pH-regulating, and acidifying agent across food, feed, and industrial applications. Its combination of acetic acid functionality and sodium acetate provides effective control of microbial growth while supporting formulation stability. The 99% purity specification offers consistent performance for industrial-scale processing and standardized formulations. Its broad utility and dependable functionality make it a commercially important ingredient for manufacturers seeking reliable acidification and preservation solutions.
2. Key Specifications & Technical Characteristics
- Chemical composition: Sodium diacetate
- Purity: 99%
- Grade: High-purity industrial/commercial grade
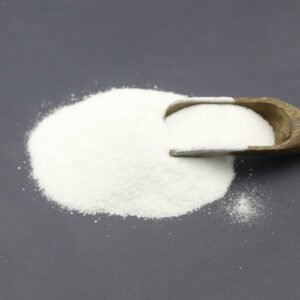
- Physical form: White crystalline powder
- Appearance: Free-flowing white powder/crystalline material
- Functional characteristics: Acidifying, buffering, antimicrobial and preservative functionality
- Packaging: 25kg bags
- Shelf life: Typically 24 months when stored under recommended conditions
- Storage: Keep tightly sealed in a cool, dry, well-ventilated environment away from moisture
- Origin: Available according to supplier production and sourcing requirements
3. Core Industrial Applications
- Food processing: Used as an acidulant, preservative, pH regulator, and antimicrobial ingredient in processed foods and bakery applications.
- Animal feed: Supports feed preservation and helps manage microbial stability in formulated feed products.
- Meat and poultry processing: Applied in formulations where controlled acidity and microbial management are commercially important.
- Bakery and processed foods: Helps extend product stability while supporting consistent formulation performance.
- Industrial formulations: Used where controlled acidity, buffering capacity, and reliable sodium acetate functionality are required.
Its combined acidifying and antimicrobial properties can provide practical formulation advantages compared with using individual acetate or acid components separately, supporting process consistency and efficient ingredient management.
4. Competitive Advantages
- Quality consistency: 99% purity supports repeatable performance across production batches.
- Supply reliability: Suitable for bulk procurement programs and ongoing industrial sourcing.
- Logistics capability: 25kg bag packaging facilitates handling, warehousing, palletization, and international shipment.
- Price competitiveness: Bulk sourcing can support efficient procurement economics for commercial-scale users.
- Sustainability: Efficient formulation performance can help reduce unnecessary ingredient consumption and support optimized manufacturing processes.
- Technical documentation: Product specifications, quality documentation, and supporting commercial information can be provided according to buyer and application requirements.
- Strategic sourcing value: Combines high purity, versatile functionality, standardized packaging, and scalable supply for professional B2B procurement.
5. Commercial & Supply Information
- Minimum Order Quantity (MOQ): BULK 20 MT
- Loading Capacity: Subject to container type, packaging configuration, applicable weight restrictions, and shipping requirements
- Packaging: 25kg bags
- Supply: Bulk and contract supply available subject to order requirements


Reviews
There are no reviews yet.