
1. Product Overview
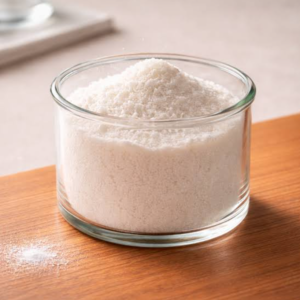
Sorbitol Powder 99% is a high-purity crystalline polyol widely used as a functional sweetener, humectant, stabilizer, and formulation aid across food, pharmaceutical, personal care, and industrial applications. Its excellent moisture-retention, solubility, and formulation properties support consistent product performance and extended shelf stability. Supplied at 99% purity, it provides manufacturers with a reliable, versatile ingredient for high-volume production. Its broad cross-industry demand makes it a strategically important commodity for efficient bulk sourcing.
2. Key Specifications & Technical Characteristics
- Chemical composition: Sorbitol (D-glucitol)
- Purity: 99%
- Grade: High-purity powder
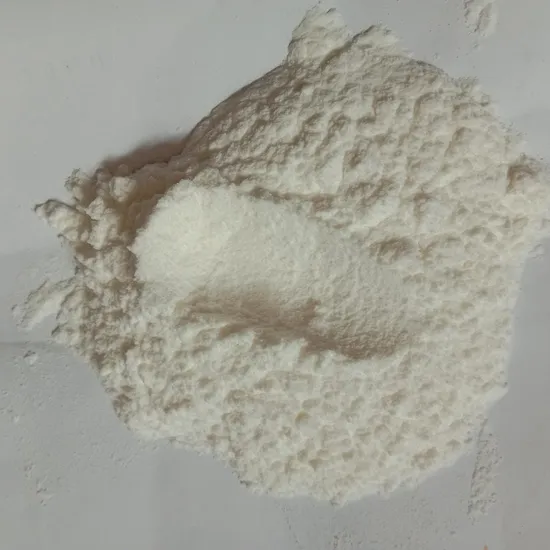
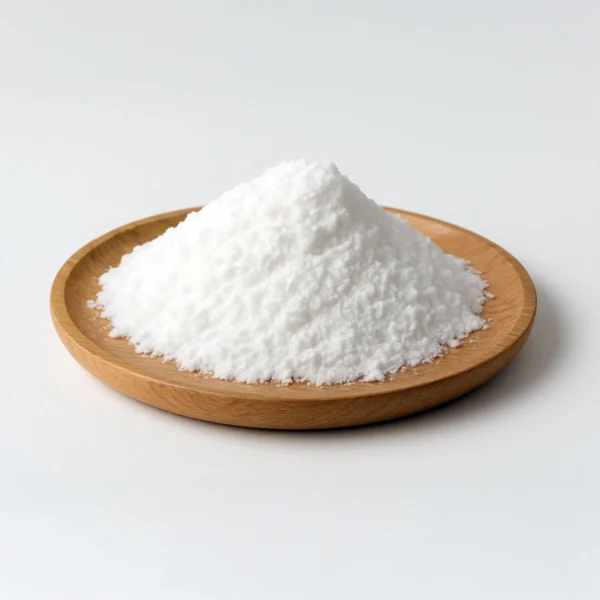
- Physical form: White crystalline powder
- Solubility: Highly soluble in water
- Functional properties: Humectant, sweetener, stabilizer, and bulking agent
- Packaging: 25 kg bags
- Shelf life: Typically 24 months when stored under recommended conditions
- Storage: Cool, dry environment in tightly sealed packaging
- Origin: Subject to supplier availability and commercial specification
3. Core Industrial Applications
- Food & Beverage: Sugar-free confectionery, chewing gum, bakery products, beverages, and functional foods.
- Pharmaceuticals: Tablet formulations, syrups, oral-care products, and excipient systems.
- Personal Care: Toothpaste, mouthwash, creams, lotions, and moisture-retaining formulations.
- Industrial Formulations: Used where controlled sweetness, moisture retention, solubility, and formulation stability are required.
- Performance advantages: Provides consistent functionality, good moisture management, and formulation flexibility compared with conventional sugar-based ingredients.
4. Competitive Advantages
- Quality consistency: 99% purity supports dependable batch-to-batch formulation performance.
- Supply reliability: Suitable for recurring industrial and bulk procurement programs.
- Logistics capability: Standard 25 kg bags facilitate handling, warehousing, and containerized international shipment.
- Price competitiveness: Bulk sourcing supports cost-efficient procurement for commercial manufacturers.
- Versatility: Broad applicability across food, pharmaceutical, personal care, and industrial sectors.
- Documentation: Technical specifications and quality documentation can be provided subject to supply arrangement.
5. Commercial & Supply Information
- Minimum Order Quantity (MOQ): BULK 20MT
- Loading Capacity: Approximately 20–25 MT per 20ft container, subject to packaging configuration and applicable loading limits
- Packaging: 25 kg bags

Reviews
There are no reviews yet.