
1. Product Overview
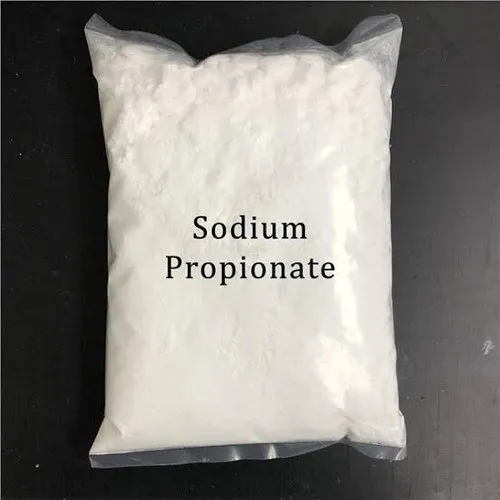
Sodium Propionate 99% is a high-purity sodium salt of propionic acid, supplied as a reliable preservative and functional ingredient for food, feed, and industrial applications. It is primarily used to inhibit mold and microbial growth, helping extend product shelf life and maintain quality during storage and distribution. With 99% purity, it provides consistent performance and dependable formulation control for commercial-scale operations. Its broad utility and efficient preservation properties make it a valuable sourcing option for manufacturers seeking reliable, cost-effective preservation solutions.
2. Key Specifications & Technical Characteristics
- Product: Sodium Propionate
- Chemical Formula: C₃H₅NaO₂
- CAS Number: 137-40-6
- Purity: ≥99%
- Grade: Food/Industrial grade, subject to applicable specification
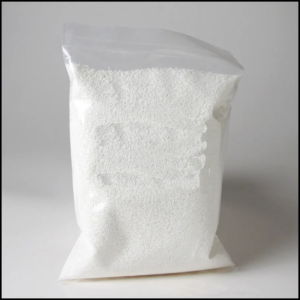
- Physical Form: White crystalline powder or granules
- Appearance: White to off-white
- Solubility: Readily soluble in water
- Packaging: 25 kg bags
- Shelf Life: Typically 24 months when stored under recommended conditions
- Storage: Keep tightly sealed in a cool, dry, well-ventilated area away from moisture and incompatible materials
- Origin: Available from international commercial supply sources
3. Core Industrial Applications
- Food Manufacturing: Used as an antimicrobial preservative, particularly in bakery products, to help control mold growth and extend shelf life.
- Animal Feed: Applied as a preservative and mold-control ingredient in feed and feed-related formulations.
- Bakery Products: Supports protection against mold development while helping maintain product quality during storage and distribution.
- Industrial Formulations: Used where controlled preservation and antimicrobial functionality are required.
- Commercial Processing: Its high purity and water solubility support efficient incorporation into large-scale manufacturing processes.
Its effective mold-inhibition properties, ease of formulation, and consistent 99% purity can provide dependable preservation performance while supporting efficient inventory and production management.
4. Competitive Advantages
- High Purity: 99% specification supports consistent formulation and predictable performance.
- Quality Consistency: Suitable for commercial applications requiring repeatable batch performance.
- Supply Reliability: 25 kg commercial packaging supports organized bulk procurement and industrial inventory planning.
- Logistics Capability: Bulk-order supply can support international B2B purchasing and containerized shipments.
- Price Competitiveness: Suitable for cost-conscious manufacturers seeking efficient preservation ingredients at commercial volumes.
- Operational Efficiency: Easy handling and incorporation into appropriate formulations can support streamlined production processes.
- Technical Documentation: Product specifications and quality documentation can be provided according to supply and customer requirements.
- Sourcing Flexibility: Suitable for food, feed, and industrial buyers seeking a versatile preservation ingredient from a single procurement channel.
5. Commercial & Supply Information
- Packaging: 25 kg bag
- Minimum Order Quantity (MOQ): BULK 20 MT
- Loading Capacity: Approximately 20–25 MT per 20-ft container, subject to packaging configuration, loading requirements, and applicable weight restrictions
- Supply: Bulk international B2B supply
Reviews
There are no reviews yet.