
1. Product Overview
Orange Drink Powder Food Grade is a carefully formulated powdered beverage ingredient designed for commercial preparation of orange-flavoured drinks, instant beverages, and powdered drink mixes. It provides consistent orange flavour, colour, and soluble performance, supporting efficient large-scale beverage production and food-service applications. Supplied in a convenient 25kg bag, it enables streamlined handling, storage, and bulk procurement for professional buyers. Its consistent formulation makes it a practical sourcing solution for manufacturers seeking reliable beverage ingredient supply and production efficiency.
2. Key Specifications & Technical Characteristics
- Product: Orange Drink Powder Food Grade
- Grade: Food Grade
- Form: Free-flowing powder
- Flavour: Orange
- Colour: Orange or orange-toned, subject to formulation
- Composition: May include sugar or sweetener, orange flavouring, food-grade acidulants, permitted colourants, and other formulation ingredients, depending on specification
- Solubility: Designed for convenient dispersion and dissolution in beverage applications
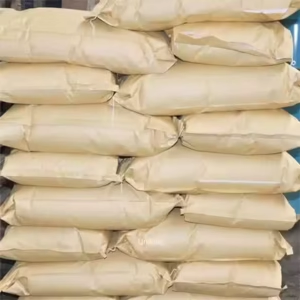
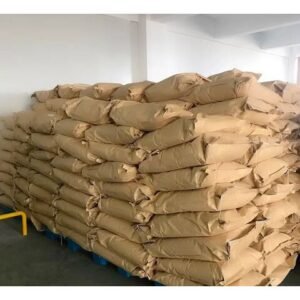
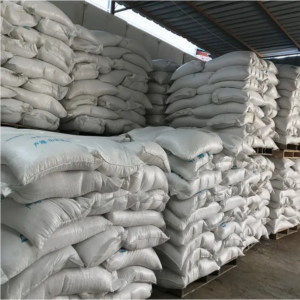
- Packaging: 25kg bags; bulk packaging options may be available subject to order requirements
- Shelf Life: Typically subject to manufacturer formulation, packaging, and storage conditions
- Storage: Store in a cool, dry environment, protected from moisture, heat, direct sunlight, and contamination
- Documentation: Product specification and relevant food-grade documentation available according to supply specification
3. Core Industrial Applications
- Beverage Manufacturing: Used in powdered orange drink mixes, instant beverages, and commercial drink formulations.
- Food & Beverage Processing: Suitable for manufacturers producing flavoured beverage concentrates, drink bases, and consumer-ready powdered products.
- Hospitality & Food Service: Supports efficient preparation of consistent orange-flavoured beverages in hotels, restaurants, catering operations, and institutional food service.
- Private-Label Production: Suitable for businesses developing branded powdered beverage products and customized formulations.
- Commercial Blending: Its powdered format facilitates efficient batching, blending, portioning, and transportation compared with ready-to-drink liquid alternatives.
4. Competitive Advantages
- Quality Consistency: Powdered format supports controlled batching and repeatable flavour performance across production runs.
- Supply Reliability: Bulk-oriented sourcing supports planned procurement and continuity for commercial beverage operations.
- Logistics Efficiency: The 25kg bag format simplifies warehouse handling, transportation, inventory management, and bulk shipment planning.
- Cost Competitiveness: Concentrated powdered form can reduce transportation and storage requirements compared with finished liquid beverages.
- Operational Efficiency: Easy integration into beverage formulations can support streamlined commercial production and preparation.
- Technical Documentation: Product specifications and applicable food-grade documentation can be provided according to buyer requirements.
- Strategic Sourcing: Suitable for manufacturers, distributors, wholesalers, and food-service buyers seeking dependable bulk beverage ingredient procurement.
5. Commercial & Supply Information
- Minimum Order Quantity (MOQ): BULK 20MT
- Loading Capacity: Subject to packaging configuration, container type, and applicable weight restrictions
- Packaging: 25kg bags
- Supply: Bulk commercial quantities available
Reviews
There are no reviews yet.