
1. Product Overview
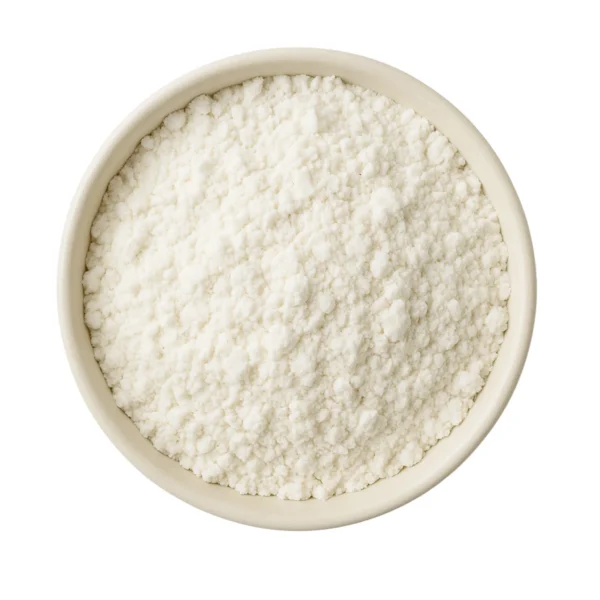
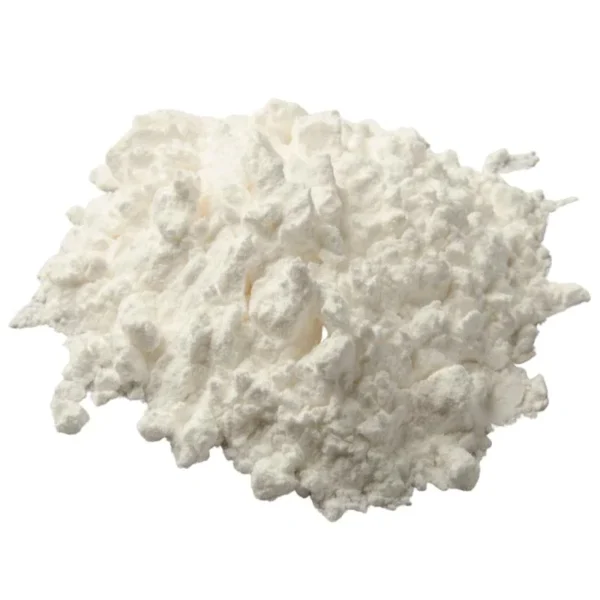
Cream of Tartar Food Grade is high-purity potassium bitartrate (potassium hydrogen tartrate), supplied as a fine white crystalline powder for professional food manufacturing and processing applications. It is widely used as an acidulant, stabilizer, leavening aid, and pH-control ingredient in bakery, confectionery, beverage, and food-processing formulations. Its consistent functional performance supports reliable production quality, formulation control, and efficient batch processing. Supplied in bulk 25kg bags, it provides a practical solution for commercial and industrial-scale sourcing.
2. Key Specifications & Technical Characteristics
- Chemical Composition: Potassium bitartrate / Potassium hydrogen tartrate (KHC₄H₄O₆)
- Grade: Food Grade
- Purity: Typically ≥99% potassium bitartrate, subject to specification and applicable food-grade standards
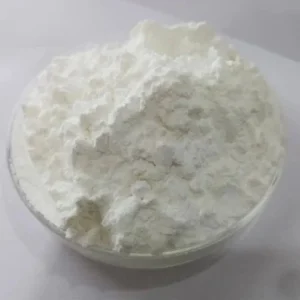
- Physical Form: Fine crystalline powder
- Color: White to off-white
- Functionality: Acidulant, stabilizer, leavening aid, pH regulator, and processing aid
- Solubility: Soluble in water, with performance dependent on formulation and processing conditions
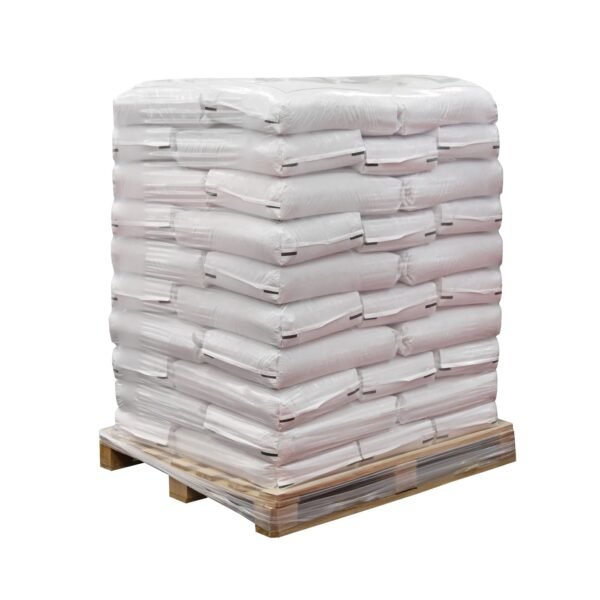
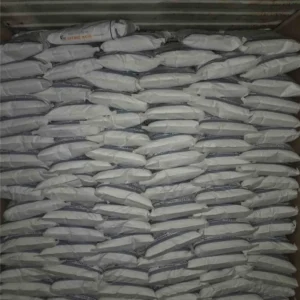
- Packaging: 25kg industrial-grade bags; customized bulk packaging may be available subject to order requirements
- Shelf Life: Typically up to 24 months when stored in a cool, dry environment in sealed original packaging, subject to supplier specification
- Storage: Keep tightly sealed and protected from moisture, heat, and contamination
3. Core Industrial Applications
- Bakery Products: Used in baking powder systems and formulations to support controlled leavening and consistent product texture.
- Confectionery: Supports acidity control and stabilization in selected confectionery formulations.
- Food Processing: Used as an acidulant and pH-control ingredient where precise formulation performance is required.
- Beverage Manufacturing: Applicable in selected formulations requiring controlled acidity and stabilization.
- Whipped Products: Helps stabilize egg whites and improve consistency in meringues, desserts, and related applications.
- Commercial Food Production: Its consistent crystalline form and controlled acidity make it suitable for repeatable industrial formulations and high-volume processing.
4. Competitive Advantages
- Quality Consistency: High-purity food-grade material supports dependable formulation performance and batch-to-batch consistency.
- Supply Reliability: Bulk 25kg packaging is suited to commercial procurement, inventory planning, and regular industrial consumption.
- Logistics Capability: Standardized packaging facilitates handling, palletization, container loading, storage, and international shipment.
- Price Competitiveness: Bulk procurement can support improved purchasing economics for manufacturers, distributors, and food-processing businesses.
- Product Efficiency: Multifunctional performance as an acidulant, stabilizer, and leavening component can simplify ingredient sourcing across multiple formulations.
- Sustainability: Efficient bulk packaging and consolidated shipment options can help reduce unnecessary handling and transport requirements.
- Technical Documentation: Product specifications, quality documentation, and relevant food-grade compliance documentation can be provided subject to order and supplier requirements.
5. Commercial & Supply Information
- Minimum Order Quantity (MOQ): BULK 20MT
- Packaging: 25kg bags
- Loading Capacity: Approximately 20 MT per standard container, subject to packaging configuration, palletization, and applicable container weight limits
Reviews
There are no reviews yet.