
1. Product Overview
Freeze-Dried Instant Coffee Food Grade is a premium soluble coffee produced through freeze-drying to preserve the coffee’s natural aroma, flavor, and soluble characteristics. Designed for food and beverage manufacturers, it provides rapid dissolution and consistent performance across instant coffee products, drink mixes, vending applications, and ready-to-serve beverages. Its advanced processing delivers a rich sensory profile with efficient handling and long-term storage suitability. Supplied in bulk commercial quantities, it supports reliable sourcing for manufacturers, distributors, and international B2B buyers.
2. Key Specifications & Technical Characteristics
- Product Type: Freeze-Dried Instant Coffee
- Grade: Food Grade
- Primary Composition: Soluble coffee solids derived from roasted coffee beans
- Form: Granulated/freeze-dried soluble coffee
- Color: Brown to dark brown
- Solubility: Rapidly soluble in hot and cold water
- Aroma & Flavor: Rich, characteristic roasted coffee aroma and flavor
- Moisture: Controlled to support product stability and shelf life
- Particle Characteristics: Uniform freeze-dried granules
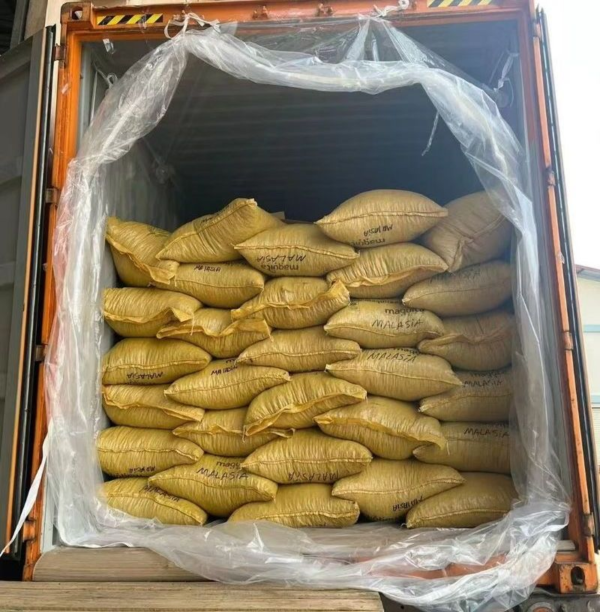
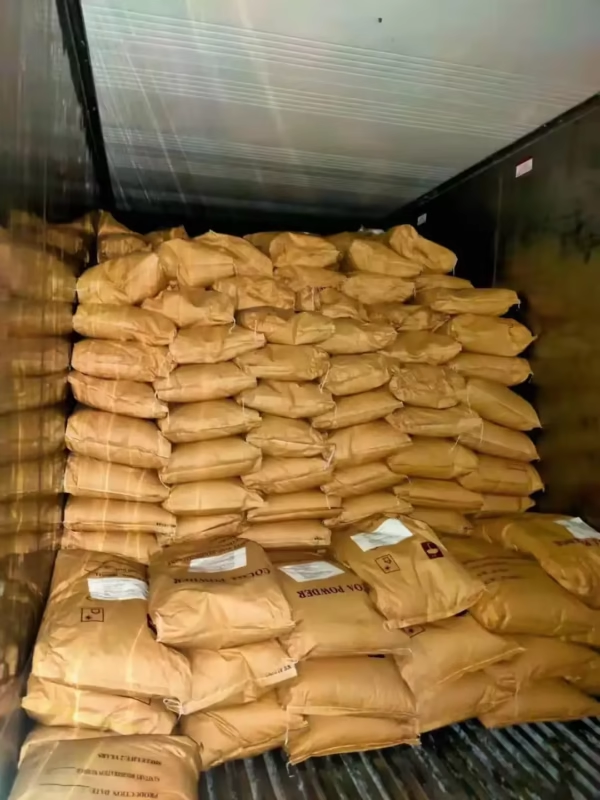
- Packaging: 20kg food-grade bags; bulk packaging available subject to specification
- Shelf Life: Typically up to 24 months when stored under recommended conditions
- Storage: Keep sealed in a cool, dry environment away from moisture, heat, and direct sunlight
3. Core Industrial Applications
- Food & Beverage Manufacturing: Used as a key ingredient in instant coffee and soluble beverage formulations.
- Ready-to-Drink Beverages: Suitable for coffee beverages, concentrates, and powdered drink systems.
- Vending & Hospitality: Provides convenient, consistent coffee preparation with rapid dissolution.
- Bakery & Confectionery: Used to deliver concentrated coffee flavor in cakes, biscuits, desserts, chocolates, and fillings.
- Foodservice & Private Label: Supports branded and private-label instant coffee production.
- Industrial Beverage Blending: Its soluble format enables efficient dosing, blending, and standardized production compared with roasted or ground coffee.
4. Competitive Advantages
- Quality Consistency: Freeze-drying helps retain desirable coffee aroma, flavor, and soluble characteristics while supporting batch-to-batch consistency.
- Supply Reliability: Structured bulk sourcing supports recurring procurement requirements for manufacturers and distributors.
- Logistics Capability: Commercial packaging is designed for efficient handling, storage, and international shipment.
- Price Competitiveness: Bulk procurement provides opportunities for competitive landed costs and scalable supply programs.
- Product Stability: Controlled moisture and appropriate packaging support extended storage and distribution.
- Sustainability: Freeze-dried soluble coffee offers efficient preparation and can reduce the need for on-site grinding and brewing operations.
- Technical Documentation: Product specifications, quality documentation, and supporting compliance information can be provided according to buyer and market requirements.
5. Commercial & Supply Information
- Minimum Order Quantity (MOQ): BULK 20MT
- Loading Capacity: Approximately 20–22 MT per 20ft container, subject to packaging configuration, product density, and applicable shipping limits
Reviews
There are no reviews yet.